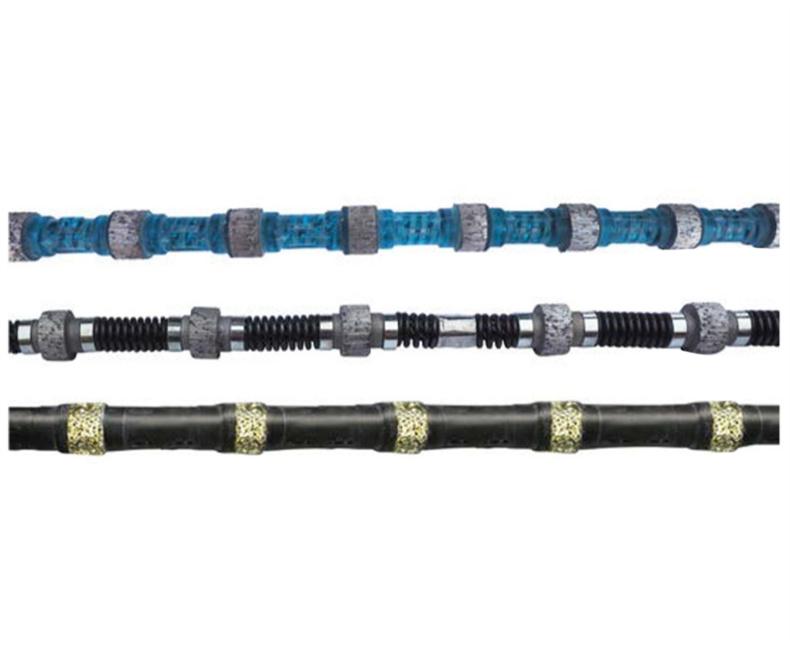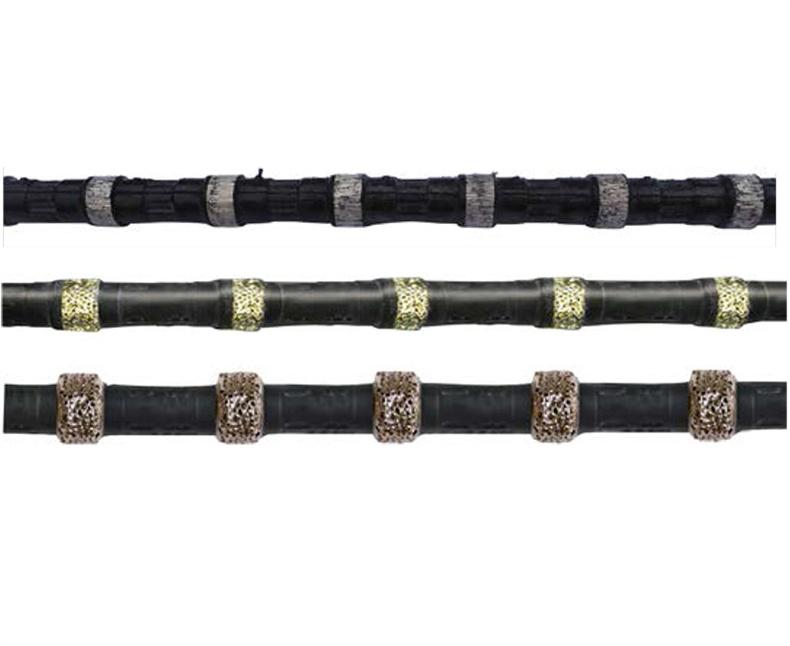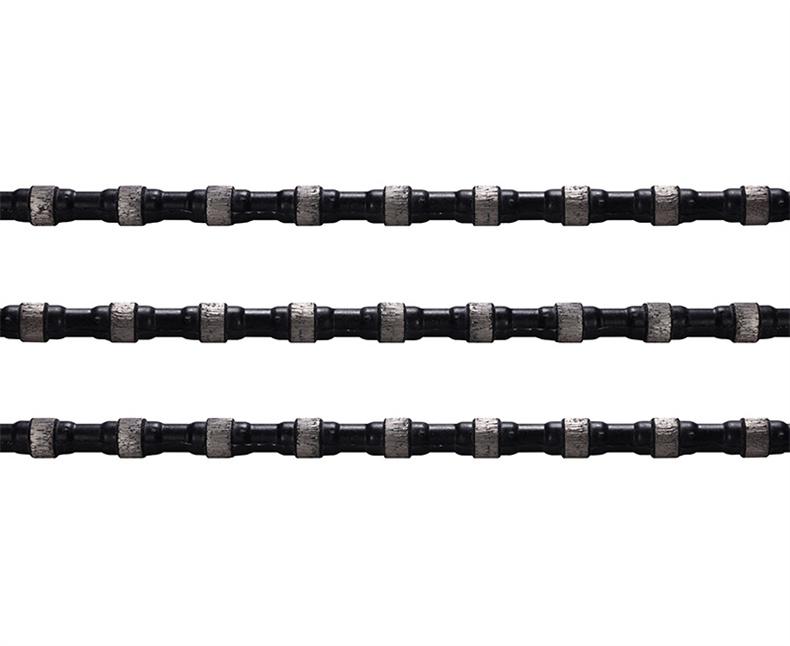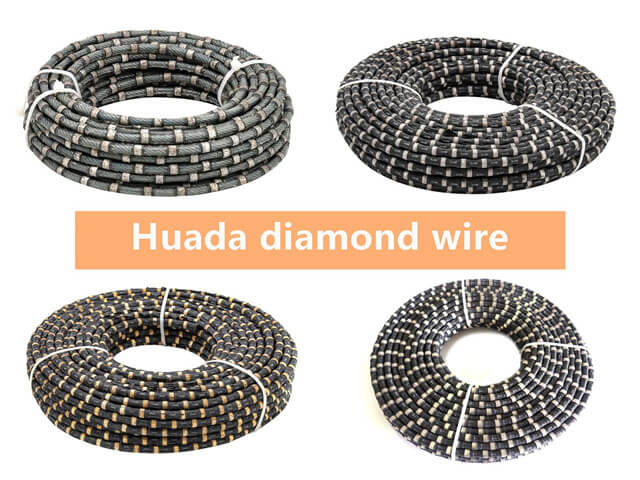


This diamond wire saw rope page contains a marble-oriented parameter set rather than one undefined rope. It separates sintered, dry-cutting and electroplated entries, with assembly and operating ranges tied to hardness and machine power.
Three bead/assembly groups
The sintered group lists Φ10.5, Φ11 and Φ11.5 mm and 33/37/40 beads per metre, with spring, rubber-plus-spring and plastic-plus-spring assemblies. The dry group lists Φ11 and Φ11.5 mm with 28/31/33 beads per metre and spring assembly. Electroplated entries use Φ10.5 or Φ11 mm with spring or rubber-plus-spring.
Hardness and motor column matter
Wire speed is shown at 35–50 m/s for one soft sintered entry and 35–45 m/s for medium/hard, dry and electroplated rows. Cutting and production values are split between 37 kW and 55/75 kW machines. The page does not support selecting one number without the construction, stone and machine column.
Rope identification sheet
- Stone sample and hardness/cutting record
- Wet or proposed dry application
- Wire-saw model and motor group
- Diameter, beads per metre and assembly
- Trial speed, cut area, time and consumption
Keep the supplied wire label with the accepted test so “diamond wire saw rope” becomes a repeatable specification. Note the new diameter before use and the measured condition at the agreed inspection point. This prevents a worn-wire measurement from being copied into a replacement order and ties consumption to the correct construction, quarry test, supplied batch identity and inspection record.