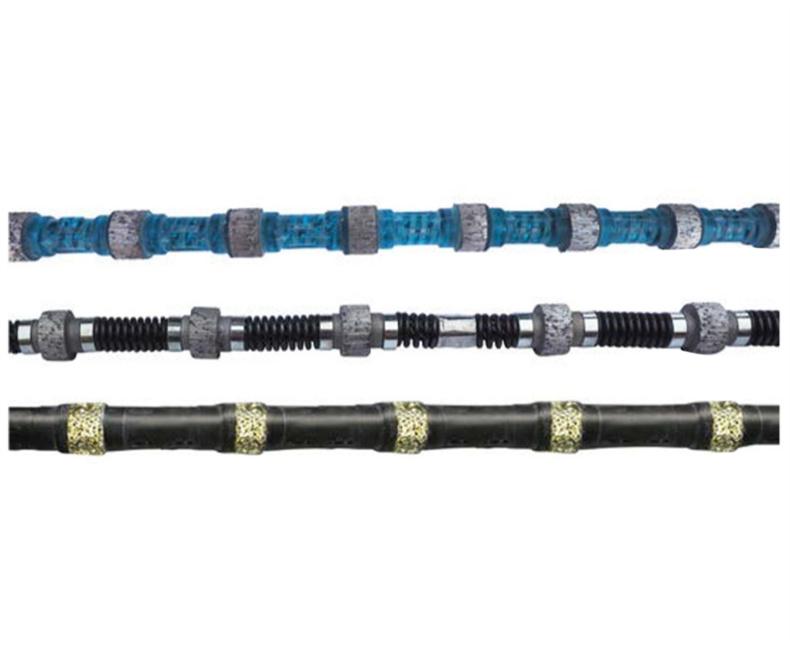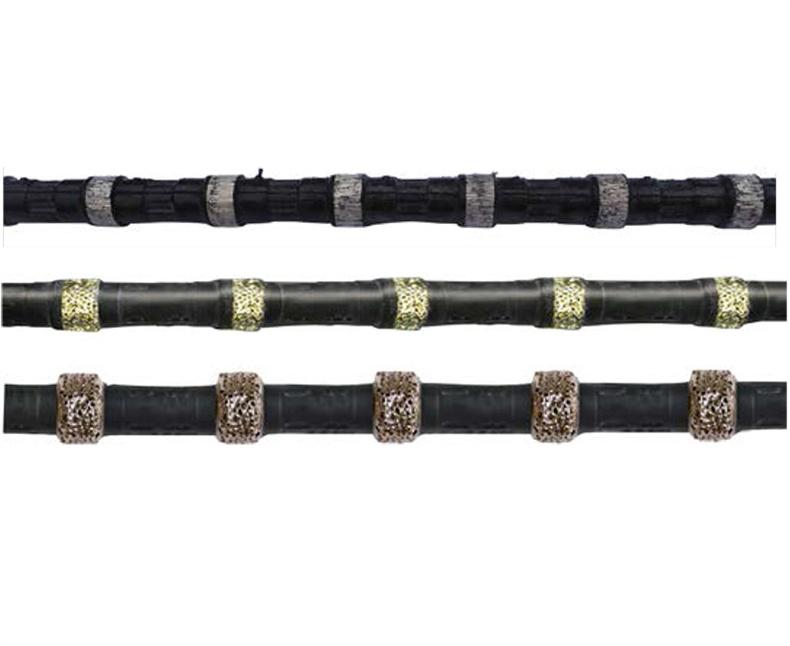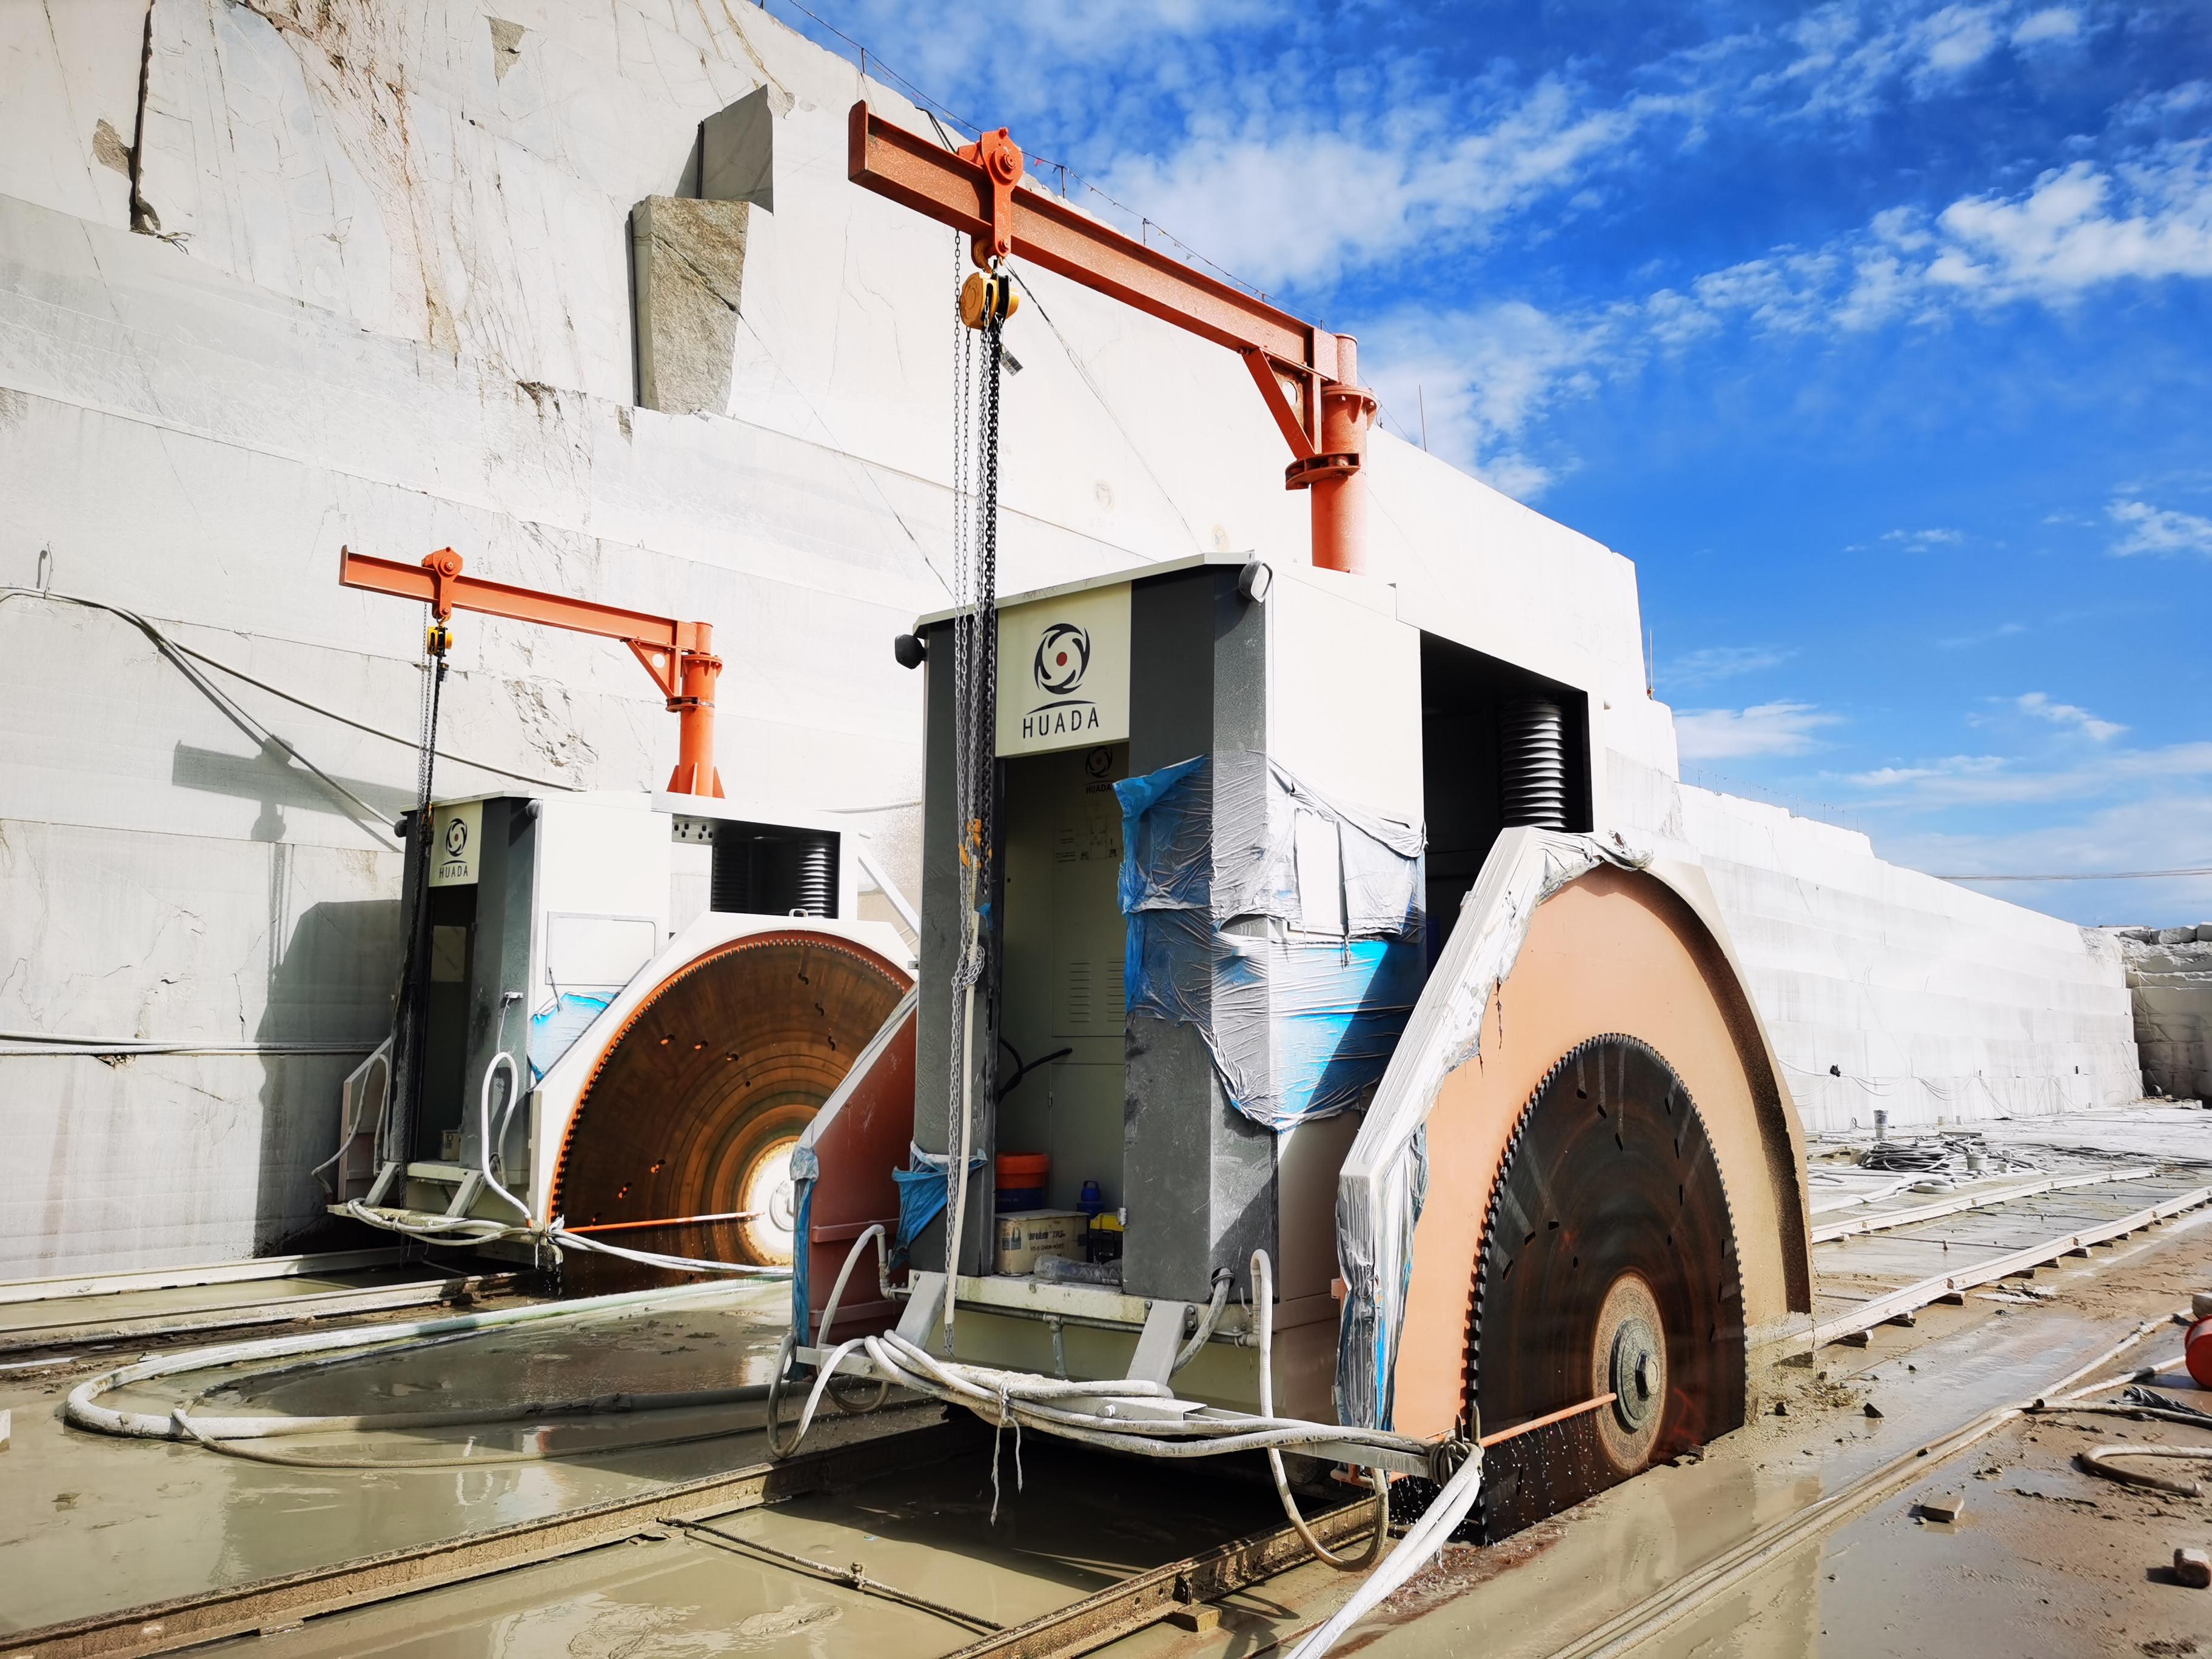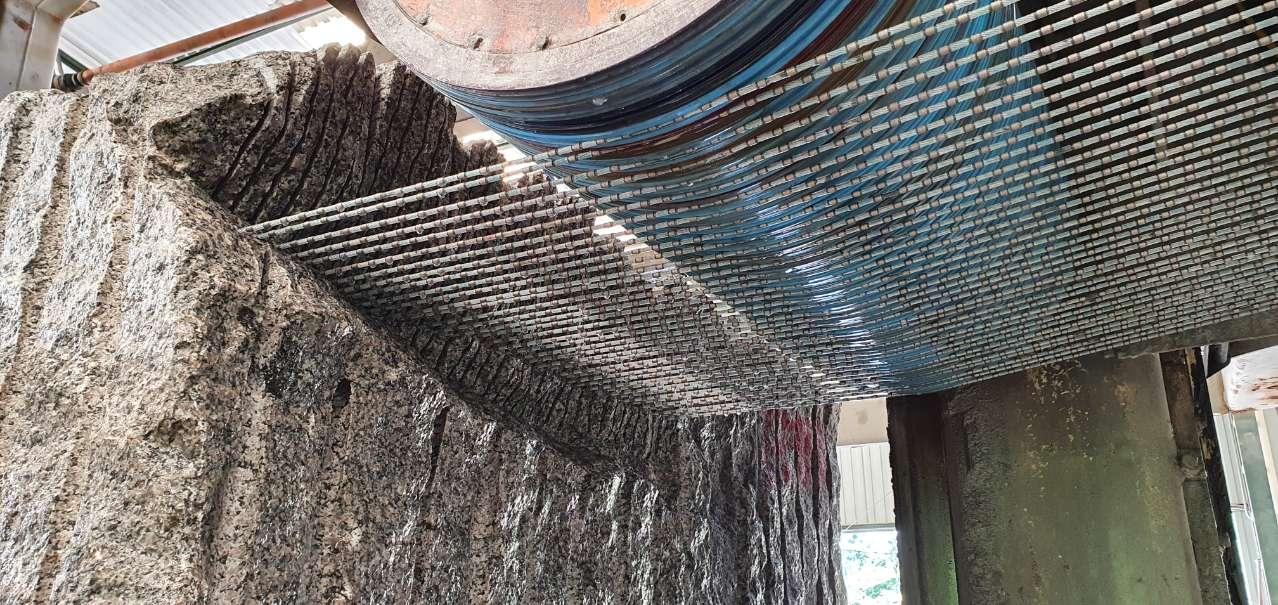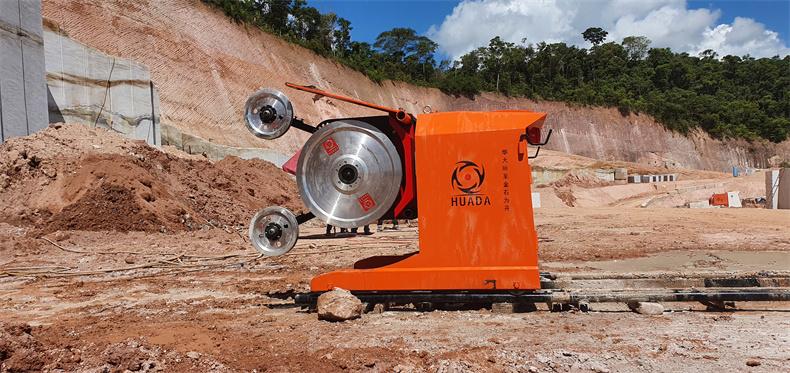


This diamond wire range is for factory block work: squaring, slab cutting and profiling. Unlike the quarry-wire pages, its old table compares granite, marble, limestone and slate and allows several assembly and diameter combinations.
Define the factory operation first
Squaring a block, cutting slabs and following a profile put different demands on the wire path and the required surface. State which operation is planned, the machine, block dimensions and the stone. The source explicitly links development to the machine, material and type of use, so one product label should not cover those inputs without review.
Material groups and source ranges
| Material | Diameter options | Beads per metre | Wire speed | Listed cutting speed |
|---|---|---|---|---|
| Granite | Φ11 / Φ10.5 / Φ9.0 / Φ8.5 mm | 35 / 37 / 40 | 26–30 or 28–30 m/s | 0.4–1.8 m²/h by hardness |
| Marble | Same listed diameters | 33 / 37 | 30–40 m/s | 3–4 m²/h |
| Limestone | Same listed diameters | 33 / 37 | 30–40 m/s | 2–3 m²/h |
| Slate | Same listed diameters | 33 / 37 | 26–35 m/s | 1–2 m²/h |
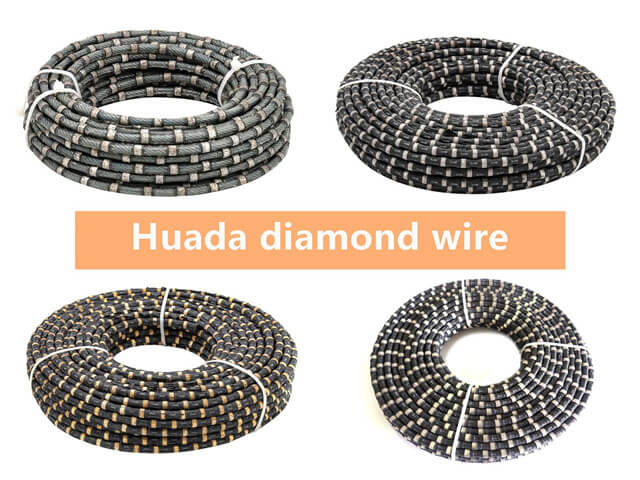
The source lists plastic, plastic-plus-spring, rubber and rubber-plus-spring assemblies. The applicable combination needs to be stated on the order.
Information for a comparable factory test
- Stone, block size and required operation
- Machine and pulley details
- Target slab or profile dimensions and finish
- Wire diameter, beads per metre and assembly
- Measured speed, cut area, accuracy and wire use
For profiling, include the drawing and acceptable deviation. For squaring or slab work, record the finished face and dimensional result on a representative block.
Original product images